Manufacturing IT Requirements for Zero Downtime
Financial Justification and Executive Case for Manufacturing IT Redundancy Network latency and system outages in manufacturing IT on the factory floor erode gross margins through adverse labor efficiency variances, unabsorbed fixed overhead, and excessive material scrap. As manufacturing environments become more dependent on integrated operational technology (OT) and enterprise resource planning (ERP) systems, the financial…
Financial Justification and Executive Case for Manufacturing IT Redundancy
Network latency and system outages in manufacturing IT on the factory floor erode gross margins through adverse labor efficiency variances, unabsorbed fixed overhead, and excessive material scrap. As manufacturing environments become more dependent on integrated operational technology (OT) and enterprise resource planning (ERP) systems, the financial controller’s mandate should extend beyond reporting to IT infrastructure resilience. A failure in data transmission during a production run can corrupt backflush costing accuracy, distort Work-in-Process (WIP) valuations, and compromise cycle counting controls.
The plan below sets out a financial and operational case for building production-grade IT redundancy, aimed at keeping production running while preserving accurate bill of materials (BOM) rollups and audit-ready records.
Scenario: Discrete Manufacturer Aluminum Casting & Whiteware Components
Context: A $45M turnover discrete manufacturing plant operating 2 shifts with 70 direct and indirect employees.
The Incident: A single point of failure (SPOF) core network switch fails due to particulate contamination from aluminum dust. Network is down for 3.5 hours.
The Financial Impact:
- Idle Labor Variance: 45 direct laborers idle. 45 workers × $32/hr burdened rate × 3.5 hrs = $5,040 unfavorable labor efficiency variance.
- Unabsorbed Overhead: Standard overhead absorption rate of $1,200/machine hour × 8 primary casting centers × 3.5 hours = $33,600 unabsorbed overhead.
- Material Scrap: Loss of temperature telemetry software during the outage results in 3 ruined batches. Standard cost materials + processing = $18,450 scrap variance.
- Total Outage Cost: $57,090 excluding delayed customer shipments and expedited freight penalties.
- CapEx Mitigation: Ruggedized edge switches in N+1 configuration cost $12,500. The ROI on this capital allocation is realized in less than one hour of prevented downtime.
Preparation Requirements for the IT Overhaul
Hardware and Facility Prerequisites: CapEx Planning
- Ruggedized Edge Servers & Switches: Use ruggedized equipment rated for dust ingress, vibration, heat, and washdown exposure as applicable to avoid premature fixed asset write-offs. Capitalize these under standard plant and equipment depreciation schedules, e.g., 5-year MACRS.
- Redundant Power UPS & Generators: Required for controlled shutdowns of CNC machines and PLC controllers, preventing physical tooling damage.
- Dual-WAN Routers: Hardware to support diverse ISP routing, such as fiber + 5G/LTE failover.
Software and Security Toolkit: OpEx / SaaS Cost Management
- Automated Failover & Monitoring Software: Tools such as PRTG are treated as OpEx. Monitoring logs can support cybersecurity insurance underwriting and SOX Section 404 internal control evidence regarding IT environment stability.
- OT/ICS Cybersecurity: Network traffic analysis helps detect lateral movement and ransomware activity that could freeze working capital by halting automated billing and dispatch workflows.
Cross-Functional Team Roles and Governance: Resource Allocation
Assemble IT architects, plant managers, and the finance team. Track internal labor hours spent coding, configuring, and testing the new architecture. Those records matter for capitalization under ASC 350-40 Internal-Use Software and for limiting avoidable OpEx.
Step 1: Assessing Manufacturing IT Requirements and Vulnerabilities
Conducting a Complete IT/OT Audit
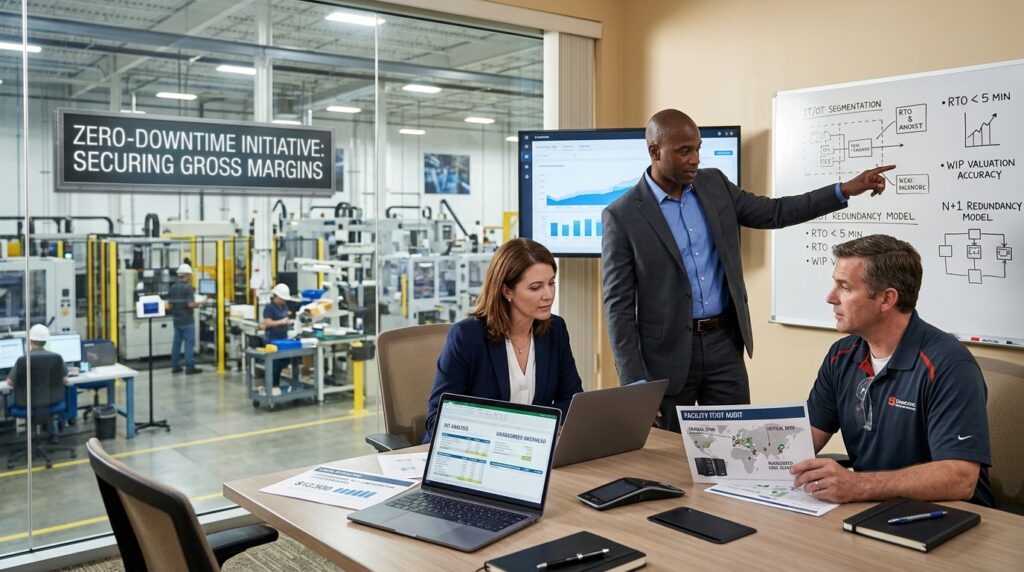
From an accounting perspective, shadow IT on the floor corrupts standard costing. Map every connected device: PLCs, MES terminals, barcode scanners. Segregate the OT network, which carries machine data, from the IT network, which carries ERP, email, and corporate traffic. When OT data flow stops, real-time WIP consumption stops. Inventory controls fail quickly, and month-end reconciliation becomes manual.
Identifying Single Points of Failure SPOF
Audit the infrastructure for bottlenecks that threaten throughput. Standalone servers hosting critical SCADA systems expose the plant to downtime, scrap, and manual control failures. Quantify the financial risk of each SPOF by calculating the hourly standard margin contribution of the work center it controls.
Establishing RPO and RTO Metrics
Translate technical metrics into financial controls:
- Recovery Point Objective RPO: Determines how much WIP transactional data is lost. An RPO of 1 hour means up to 1 hour of material consumption and labor routing transactions must be manually re-keyed, introducing human error into BOM rollups. Target RPO: Near-zero.
- Recovery Time Objective RTO: Determines the duration of unabsorbed overhead and idle labor. Target RTO: < 5 minutes via automated failover.
2: Designing and Deploying Redundant Infrastructure
Building an N+1 Network and Power Redundancy Model
Implement an N+1 redundancy framework.
- Cost Table: Redundancy vs. Downtime Avoidance
| Infrastructure Layer | CapEx Investment | Monthly Depreciation 60 mo | Prevents per incident | Break-Even Outages |
|---|---|---|---|---|
| Dual ISP / Firewalls | $8,000 | $133 | $12,000 Idle Labor/OH | 0.66 |
| Ruggedized Edge Nodes | $15,000 | $250 | $18,450 Scrap Variance | 0.81 |
| Plant Floor UPS Systems | $22,000 | $366 | $45,000 Tooling Damage | 0.48 |
Implementing Edge Computing and Cloud Failovers
Keep MES and SCADA processing at the edge, on the factory floor. If the external cloud ERP connection drops, the edge server buffers barcode scans, cycle counts, and labor time-clock punches. Once the connection returns, data syncs using FIFO logic. This preserves accurate absorption costing and prevents negative inventory balances.
Stress-Testing Failover Protocols
Execute shutdown simulations during weekend maintenance windows. For the financial controller, treat this as an internal-controls audit as much as an IT exercise. Verify that standard cost variances remain unaffected during failover and that production output continues without generating false material variances.
Failure Modes to Avoid
Merging IT and OT Networks Without Proper Segmentation
The Error: Running standard corporate traffic, such as email and streaming traffic, on the same VLAN as physical machine instructions.
The Consequence: Bandwidth saturation causes packet loss to PLCs, resulting in micro-stoppages. In high-volume manufacturing, these 10-second interruptions compound and can destroy labor efficiency targets. An IT phishing breach can also traverse to the factory floor, halting operations entirely.
Underestimating the Factory Floor Environment Asset Write-Offs
The Error: Choosing standard office-grade servers because the upfront CapEx is lower, then installing them in a dusty, un-air-conditioned plant floor environment.
The Consequence: Heat and particulate ingress destroy motherboards within 14 months. Finance is forced to record early impairment charges/write-offs on fixed assets, affecting departmental P&L, while also incurring the cost of emergency replacement hardware at a premium.
Failing to Schedule Regular Disaster Recovery Drills
The Error: Treating redundancy as a sunk CapEx cost with no required maintenance.
The Consequence: During an actual failure, expired SSL certificates or unpatched firmware on the backup system can cause failover to crash. External auditors may flag this lack of IT general controls ITGC as a material weakness in financial reporting environments.
Target State: 99.99% Uptime and Production-Grade Operations
Continuous Production
In the target state, failover is tested, documented, and treated as an operating control. The immediate financial outcome is stabilization of standard cost variances. When fixed overhead absorption becomes predictable, margin analysis becomes more reliable, supporting better pricing decisions during customer contract negotiations.
Early-Warning Monitoring and Alerting
Integrated network monitoring flags capital asset degradation early. By monitoring the thermal output and CPU loads of OT servers, plant maintenance can execute predictive hardware replacements during scheduled downtime. The cost profile shifts from unpredictable emergency OpEx to planned CapEx.
Scalability for Additional Automation
Resilient infrastructure is required before the plant adds automation that depends on continuous network and system availability. With tested uptime controls and segmented networks, the plant can securely integrate AI-driven visual quality inspection and automated guided vehicles AGVs, reducing direct labor costs and improving standard margins over time.
Frequently Asked Questions
What are the minimum Manufacturing IT Requirements for a mid-sized plant?
For a $20M–$60M plant, the minimum requirements are physically segmented IT/OT VLANs, ruggedized network switches on the floor, UPS backups for all critical PLCs, and automated off-site daily backups of the ERP and MES databases to protect accounts receivable and WIP ledgers.
How does infrastructure redundancy affect production ROI?
Return on Investment ROI is generated primarily through cost avoidance. If a plant operates at a $50,000/hour downtime burn rate comprising unabsorbed overhead, idle labor, and lost contribution margin, a $40,000 redundancy CapEx investment pays for itself during the first 48 minutes of prevented downtime. The IRR depends on outage frequency and avoided downtime cost.
What is the difference between IT and OT uptime strategies?
IT uptime protects transactional data integrity: ERP access, email, AR/AP workflows. In that environment, a 5-second latency delay is usually an inconvenience. OT uptime protects real-time deterministic control of physical machinery; the same delay can cause a robotic welder to miss a seam, creating immediate scrap, safety risk, and irreversible material variances. OT redundancy requires rapid, low-latency failover.